
Case Study · Pet Food
Turn-key Pet Food Rendering Solution
Partnering with an OEM to automate the meat processing operation.
Project Summary
Bachelor Controls' work with The Williams-Carver Company is a unique situation: BCI is three levels removed from actually working with the end-user plant. That level of project complexity requires excellent communication and exceptional domain expertise to execute well.
Williams-Carver offers this BCI-provided solution to a food and beverage processing company's end-users as a turn-key solution. The end-user plants process by-product from the pork industry to be sold as fresh pet food.
Challenge
Williams-Carver, a sanitary stainless and refrigeration distributor, was hired by a world-renowned food and beverage processing company to provide a turn-key automated system for processing meat, which was formerly a 100% manual process. Williams-Carver developed the process system and supplied the majority of the hardware, and Bachelor Controls was brought in to design and implement the controls that automate the process.
Beyond the efficiencies gained through automation, another critical feature was upgrading the historian and reporting functions of the system, which formerly used either a hand-written clipboard or a manual chart recorder that logged the temperature to a circular chart.
Bachelor Controls is very knowledgeable in what they do, they are easy to work with and they care about their end product.
Solution & Benefits
BCI designed an Allen-Bradley CompactLogix system with FactoryTalk View SE HMIs. Services included the electrical design, programming, schematics and panel drawings, and panel builds.
When converting the system to CompactLogix with FactoryTalk View SE HMI, BCI wrote a data application to log the temperatures to a SQL database on the PC. Operators can now print and ship a report with the product instead of sending a hand-written log of time and temperature. BCI supplies the custom-developed and proprietary data logger application with all of these solutions.
One of the end-user plants preferred a Schneider Electric PLC and Inductive Automation Ignition HMI platforms, so BCI converted the Allen-Bradley solution to accommodate that preference.
For the panel build, every system had one main panel to house the PLC, the drives, and the motor starters. Some panels were customized with an attached HMI, and other panels had the HMIs independently located on the plant floor. Every system on the plant floor was housed in a NEMA 4x.
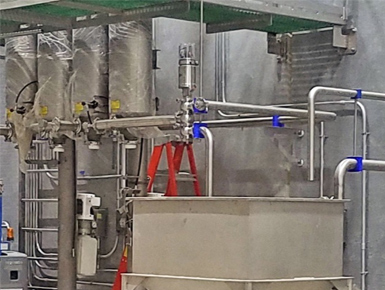
To achieve the correct product cooling, BCI worked with Williams-Carver to install and control multiple SPX Flow Votators. These are scraped surface heat exchangers which cool the product from about 102F to about 32F. Based on the product mix and density, Williams-Carver provides the proper quantity of Votators based upon max product flow in lbs./hour to meet that cooling rate.
Results
5 yrs
Temperature data retained
102°F → 32°F
Controlled product cooling
How the System Runs
The fully automated system produces a better and more consistent quality product with better controls for the end-user, and automatically records the temperature of the product as it goes through the system. The control system allows the product to cool to the ideal temperature without freezing it, which had been a problem with previous systems.
From receiving the by-product to loading the rendered pet food onto the shipping truck, this BCI turn-key solution provides a data log that records the temperature of the product accurately at various points throughout the operation. That data can be referenced as far back as 5 years, aiding in the temperature auditing process.
Automation also allows for alerting features. For example, the system warns the operator when the truck is nearly full. Then, when the full setpoint is reached, the system automatically shuts down and blows the line out.
- Data log program automatically records temperature of product accurately
- Fully automated system controls product temperature more efficiently
- Customized panel build to house the PLC, drives and motor starters
Automating an OEM's Process System?
We work well several levels removed from the plant floor. Tell us about the system.